We manufacture both epoxy and cementitious grout, and "wind turbine foundation grout" is one of the most confused specifications that reaches our inbox — usually because the enquiry starts from an epoxy grout data sheet used for pumps and compressors, then gets applied to a completely different structural problem. This guide separates the two real cases: onshore tower base grouting, and offshore monopile grouted connections.
Why a Wind Turbine Foundation Needs Grout At All
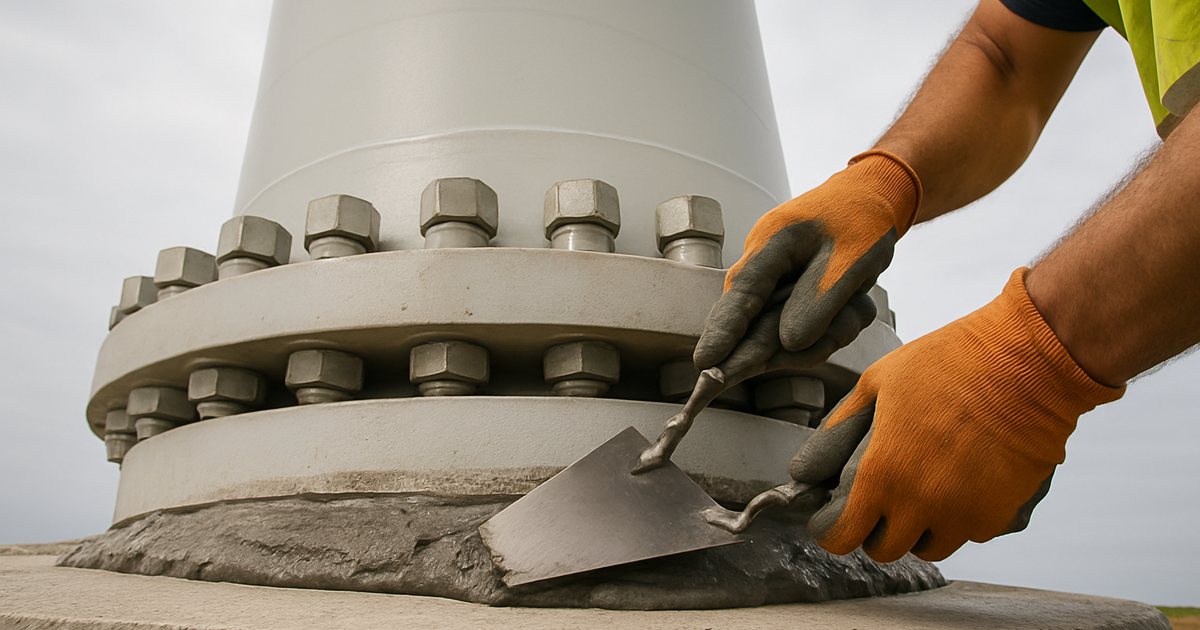
A wind turbine tower is not bolted directly to concrete. Loads — a static weight of 150–400 tonnes for the tower and nacelle, plus large cyclic bending moments from wind and rotor thrust — have to transfer from a circular steel flange (onshore) or a tubular steel monopile (offshore) into a concrete or seabed foundation. The interface between dissimilar materials, steel and concrete, is never perfectly flat or perfectly aligned. Grout is the load-transfer layer that:
- Fills the gap left by fabrication and installation tolerances so the full flange bears evenly, not just at a few high points.
- Transfers compressive and shear load into the concrete without stress concentrations.
- Must survive 10 million-plus load cycles over a 20–25 year design life without losing bond, cracking through, or settling.
Onshore Tower Base: Cementitious Grout Is the Standard, Not Epoxy
We get a steady stream of enquiries for "wind turbine foundation epoxy grout," and it is worth correcting directly: epoxy grout is the wrong material for the tower base ring in almost every onshore case.
| Property | Cementitious Grout (60–80 MPa) | Epoxy Grout |
|---|---|---|
| Typical pour thickness | 50–150 mm, several m³ per tower | Limited to ~100 mm per lift |
| Exotherm risk on thick pour | Low — mix design controls heat of hydration | High — can exceed 90 °C in a thick section, cracking the grout |
| Coefficient of thermal expansion vs. concrete | Closely matched (~10–12 × 10⁻⁶/°C) | Mismatched ~2.5:1 (~25–30 × 10⁻⁶/°C) |
| Flowability under a large flange | Self-levelling, pumpable, flow-cone controlled | Thixotropic, harder to place in large volume |
| Material cost for a full tower base (2–4 m³) | Moderate | 4–6× cementitious cost — indefensible at this volume |
| Compressive strength achievable | 60–80 MPa (28 d), non-shrink | ≥ 80 MPa, but strength is not the limiting factor here |
| Correct use on a wind turbine | Tower base flange / embedment ring | Nacelle-side equipment — yaw drive, gearbox, generator baseplates |
The one governing reason is volume and heat: a pump baseplate takes litres of grout; a 4–4.5 m diameter tower base ring takes cubic metres. Epoxy resin curing is exothermic, and in a thick, large-volume pour that heat cannot escape fast enough — internal temperatures climb, and the grout cracks itself apart during cure. Cementitious grout's heat of hydration is an order of magnitude lower and is manageable with standard mix design (low-heat cement blend, controlled water content, sometimes ice water in hot climates).
Specification checklist for onshore tower base grout
- Compressive strength: ≥ 60 MPa at 28 days per ASTM C1107 (non-shrink hydraulic cement grout) or EN 12190 (cementitious repair products)
- Flow: measured by flow-cone time — typically 15–35 seconds depending on channel geometry and pumping distance
- Shrinkage: non-shrink, expansive-additive formulation; volumetric change within ±0.05% per ASTM C1090
- Early-age movement: relative movement between flange and grout during initial cure should not exceed 1 mm — this threshold, drawn from DNV-ST-0126's early-age cycling limit for offshore connections, is good onshore practice too, since bolt-up and crane operations can transmit vibration into a still-curing pour
- Compatibility: coefficient of thermal expansion within roughly 20% of the surrounding foundation concrete
Offshore Monopile Grouted Connections: A Different Engineering Problem
Offshore wind changes the geometry entirely. Instead of a flange sitting on a concrete pad, a monopile is driven into the seabed and a transition piece slides over the top of it, leaving an annular gap of typically 40–100 mm that is filled with grout over a length of several metres. This grouted connection has to transfer both the static and cyclic loads of the entire tower and turbine into the pile, underwater, for the life of the asset.
> Field lesson the whole industry learned the hard way: toward the end of 2009, operators across a significant share of the installed European offshore fleet began reporting grouted connections slipping downward, with cracking near the top and bottom grout seals. DNV ran a joint industry project from late 2009 through January 2011 and found that axial capacity of a plain (unkeyed) grouted connection was far more sensitive to pile diameter and surface tolerance than the design codes of the time assumed. The fix, now written into DNV-ST-0126, is mandatory shear keys — raised weld beads on both the pile and transition-piece surfaces — which testing showed increase axial capacity roughly six-fold compared to a plain connection.
That single design change is why every current-generation monopile foundation has visible weld-bead shear keys inside the grouted annulus, and why any retrofit or life-extension project on a pre-2011 turbine needs an axial capacity check against DNV-ST-0126 before assuming the original grout connection is adequate for another design life.
What offshore monopile grout must achieve
- Compressive strength ≥ 80–100 MPa — offshore connections are specified higher than onshore tower bases because the annulus is narrower and the connection is fatigue-critical, not just statically loaded
- Anti-washout performance: grout is placed via tremie pipe into an annulus that may have residual seawater present, so the mix must resist washout and maintain strength — the same anti-washout chemistry we use in our underwater grout XQ-GJ-UW, covered in more depth in our underwater concrete placement guide
- Fatigue performance under 10⁷+ cycles, verified per DNV-ST-0126 fatigue test protocols
- Early-age cycling tolerance: relative movement during initial cure capped at 1 mm, because vessel motion and pile driving of adjacent foundations can transmit vibration through the seabed during the curing window
- Bleed and segregation control, since the pour is effectively invisible once placed — there is no chipping back and re-pouring a bad batch at 25 m water depth
Diagnosing and Repairing Cracked or Settled Foundation Grout
For turbines already in service, the practical question is rarely "which grout to specify" — it is "why is this one failing, and can it be fixed without a full foundation rebuild." Three failure patterns account for most of what we see referred to us by O&M contractors:
Repair strategy depends on which pattern is present, confirmed by hammer sounding, ultrasonic survey, or (for offshore assets) diver inspection:
| Failure pattern | Repair approach | Feasible without full unbolt/lift? |
|---|---|---|
| Voiding / debonding, grout body still sound | Pressure injection of low-viscosity epoxy or cementitious grout through drilled ports | Yes |
| Radial cracking, grout body still bonded | Surface-seal crack injection, then monitor | Yes |
| Settlement / slip, load path compromised | Remedial shear-key installation + full re-grout, or supplementary steel bracket system | Usually no — engineered repair design required |
Our approach to voided or debonded grout mirrors the pressure-injection method in our machinery foundation grout guide: drill 10 mm ports at 300–400 mm centres into the void, seal the perimeter, and inject a 200–400 mPa·s injection grout from the lowest port upward until it appears at the next port. The same low-viscosity, bottom-up sequencing used for concrete crack injection applies here at a larger scale.
Volume and Cost: Sizing a Tower Base Pour
For a typical onshore tower with a base flange diameter of 4.0–4.5 m and a grout channel 100 mm deep by 150 mm wide:
Volume (litres) ≈ π × D(average) × channel width × channel depth × 1000 × 1.15For a 4.2 m average diameter ring, 0.15 m wide, 0.10 m deep: π × 4.2 × 0.15 × 0.10 × 1000 × 1.15 ≈ 228 litres per tower base — call it roughly 480 kg of dry cementitious grout mix at a typical 2.1 kg/L density. The 1.15 factor covers waste, over-break, and topping-up around anchor cage penetrations.
| Item | Cementitious grout (60–80 MPa) | Epoxy grout (for comparison only — nacelle equipment, not tower base) |
|---|---|---|
| Typical FOB Ningbo price | USD 0.35–0.70 /kg | USD 3.20–5.60 /kg |
| Packaging | 25 kg bags, or 1-tonne bulk bags for large wind farm orders | 25 kg three-component sets |
| MOQ | 1,000 kg (a partial container for a small order; full 20 ft container for wind farm-scale projects) | 500 kg (20 sets) |
| Standard lead time, FOB | 10–15 days | 12–18 days |
| Typical order size, 20-turbine onshore project | 8–10 tonnes | Not applicable at tower base |
For offshore projects, grout volumes scale with pile diameter and annulus length rather than a flat ring, and are normally quoted per project after we receive the pile and transition-piece drawings — annulus lengths of 3–8 m are common, and total grout volume per foundation typically runs into several tonnes.
Common Specification Mistakes We See
- Copying a machinery-grout spec sheet onto a wind turbine tender. The 80 MPa epoxy spec that is correct for a compressor skid is the wrong document for a tower base — see the comparison table above.
- Assuming a pre-2011 offshore turbine's original grout design is still adequate. If shear keys were not part of the original connection, an axial capacity recheck against DNV-ST-0126 is the first step before any life extension or repowering decision.
- Skipping the early-age movement check. Both onshore and offshore grout are vulnerable during the first 24–72 hours; crane operations, bolt-up torquing, or adjacent pile driving within that window is the single most common avoidable cause of early cracking.
- No anti-washout provision for offshore or waterlogged onshore pours. Standard cementitious grout loses strength badly if seawater or groundwater mixes in during placement; specify an anti-washout admixture or an underwater-grade product.
Sourcing Wind Turbine Foundation Grout
We supply non-shrink cementitious grout, anti-washout underwater grout, and low-viscosity injection grout to wind farm EPC contractors and O&M service companies in more than 40 countries. Certifications supplied as standard: ISO 9001, SGS material test reports, and third-party compressive strength testing per ASTM C1107 or EN 12190 on request. Custom mix designs (extended flow time for long pumping distances, low-heat formulations for hot climates, cold-weather accelerated grades) are available from 2,000 kg.
Need a material specification for a specific project? Send us the flange diameter and channel geometry (onshore) or the pile diameter, annulus width, and length (offshore), along with the ambient and water temperature range, and our engineering team will return a mix recommendation and quantity take-off within one working day. Request a quote →Frequently Asked Questions
Q: Should I use epoxy or cementitious grout for a wind turbine tower base? A: Cementitious, at 60–80 MPa, non-shrink. The pour is too thick and too large in volume for epoxy grout to cure without exotherm cracking, and its thermal expansion is too far from that of the surrounding concrete. Reserve epoxy grout for smaller nacelle-side equipment baseplates. Q: What standard governs offshore monopile grouted connections? A: DNV-ST-0126 (Support structures for wind turbines) is the current reference, requiring shear keys in the grouted annulus following the 2009–2011 industry investigation into unkeyed connection failures. Design also needs to account with IEC 61400-3 loading and, for older assets, a specific check against the original (pre-revision) design basis. Q: Why did offshore grouted connections fail in 2009? A: Plain, unkeyed grouted connections settled and cracked across a significant part of the installed European fleet. Investigation found axial capacity was far more sensitive to pile diameter and surface finish tolerance than the contemporary design codes assumed. Adding shear keys increased tested axial capacity roughly six-fold, and shear keys are now mandatory under DNV-ST-0126. Q: Can a cracked or settled foundation grout be repaired without removing the tower? A: If the damage is voiding or debonding with the grout body otherwise sound, yes — pressure injection through drilled ports can restore the load path. If the connection has genuinely settled or slipped, that indicates the load path has already changed, and it typically needs an engineered repair (remedial shear keys, supplementary steel brackets) rather than injection alone. Q: How much grout does one onshore tower base need? A: For a typical 4.0–4.5 m diameter flange with a 100 mm deep, 150 mm wide channel, expect roughly 200–260 litres (420–550 kg) of cementitious grout mix per tower, plus an allowance for anchor cage penetrations and waste. Q: What compressive strength should I specify? A: 60–80 MPa (28-day, ASTM C1107 or EN 12190) for onshore tower bases. Offshore monopile grout is typically specified higher, 80–100 MPa, because the connection is fatigue-critical and the annulus geometry is less forgiving than an open tower base ring. Q: What is your MOQ and lead time for wind farm projects? A: 1,000 kg minimum order for cementitious grout (roughly a partial container; a full 20 ft container suits multi-turbine orders), 10–15 days lead time FOB Ningbo. Offshore-grade and anti-washout formulations are quoted per project once we have pile and transition-piece dimensions.Related Guides
- Best Epoxy Grout for Machinery Foundations
- Cementitious Grout Types, Strength and Applications
- Non-Shrink Grout: ASTM Properties and Equipment Base Selection
- Underwater Concrete Placement: Anti-Washout Tremie Methods
- Concrete Crack Injection: Methods and Materials
- Browse our full grouting material range →
*XINCHOR manufactures non-shrink cementitious grout, underwater/anti-washout grout, and injection grout for wind turbine and heavy equipment foundations, supplied to EPC and O&M contractors in more than 40 countries. Send us your foundation drawings and site conditions and we will return a material specification, quantity take-off, and FOB quotation within one working day. Contact XINCHOR — WhatsApp: +86 133 3618 3725 | Email: info@xinchor.com*